主な利点
バイヤーがこの工法を選ぶ実務的な理由。
Volume Economics
Tooling pays back at scale
Lower piece price at volume
- •Progressive options
- •Stage tools
- •High repeatability
- •Fast cycle
Feature Integration
Pierce + form in tool
Complex stamped features
- •Lances
- •Emboss
- •Countersinks
- •Forms
Consistency
Die-controlled geometry
Lot-to-lot repeat
- •Stable dims
- •Cosmetic control
- •High throughput
- •SPC friendly
Bridge Path
Laser first, stamp later
De-risk before die spend
- •Validate design in laser
- •Freeze CAD
- •Then tool
- •Cost-down plan
Secondary Ops
After stamp
Tap, plate, assemble
- •Hardware
- •Plating
- •Welding
- •Packaging
Export Lots
China production
Carton/pallet programs
- •Kanban friendly
- •Lot labels
- •FAI
- •Freight
提供内容
Tooling & Stamping
Stage or progressive tools matched to volume.
Tool quote
Die cost + piece price breaks
Sample approval
FA before volume
Maintenance
Tool care notes in program
材料
Steel, stainless, aluminum coils/sheets.
CRS / HSLA
Common structural stamps
Stainless
When corrosion needs apply
Aluminum
Lightweight brackets/panels
Finishing
Plate, coat, and assemble after stamp.
Zinc plate
Powder coat
Deburr
Hardware
業界と用途
商業・産業向け板金—規制認証の過大主張なしのソフト能力表現。
Automotive Supply
Brackets and clips—commercial programs.
- •Brackets
- •Clips
- •Shields
- •Reinforcements
Appliance / Electronics
Repeat housings and frames.
- •Frames
- •Shields
- •Mounts
- •Covers
Industrial OEM
High-volume stamped plates.
- •Washers
- •Plates
- •Links
- •Guards
Hardware / Consumer
Stamped consumer metal parts.
- •Brackets
- •Hinges
- •Plates
- •Clips
材料
常用板金グレード。厚さ・仕上げは見積で確認してください。
Stampable Metals
- • CRS
- • HSLA (select)
- • Stainless
- • Aluminum
- • Galvanized
Thickness
- • Thin gauge to mid range—per tool design
品質・検査メモ
RFQコールアウトに沿った実務QC—一括の航空宇宙主張はありません。
入荷確認
材料と造形パラメータを注文に照合
工程内確認
後処理中の重要特徴スポットチェック
最終検査
合意CTQに基づく目視+寸法注記
輸出梱包
海外輸送向け保護梱包
文書
注文時の材料注記と検査記録
当社プロセス
CADと要件提出
STEP/DXFをアップロードし材料・厚さ・仕上げ・数量を伝える
見積とDFM注記
工法提案と製造性フィードバック
加工と仕上げ
切断/成形/接合後、合意した仕上げ
検査
梱包前にCTQと外観を確認
出荷
宛先向け輸出カートン
よくある質問
When does stamping beat laser?
When annual volume makes die cost cheaper per piece than nested laser. We compare on quote.
Tool ownership?
Discussed on PO—typically buyer-owned after payment.
Lead time for tools?
Weeks depending on complexity; samples follow tool tryout.
Can you stamp then weld?
Yes—stamped components into weldments are common.
Minimum order after tooling?
Depends on setup economics—ask for lot size guidance.
認証は?
ソフト能力表現のみ。一括の航空宇宙板金認証は主張しません。
Design changes after tooling?
May require tool modification cost—freeze design before steel.
認証は?
ソフト能力表現のみ。一括の航空宇宙板金認証は主張しません。
板金プレス—サービス概要
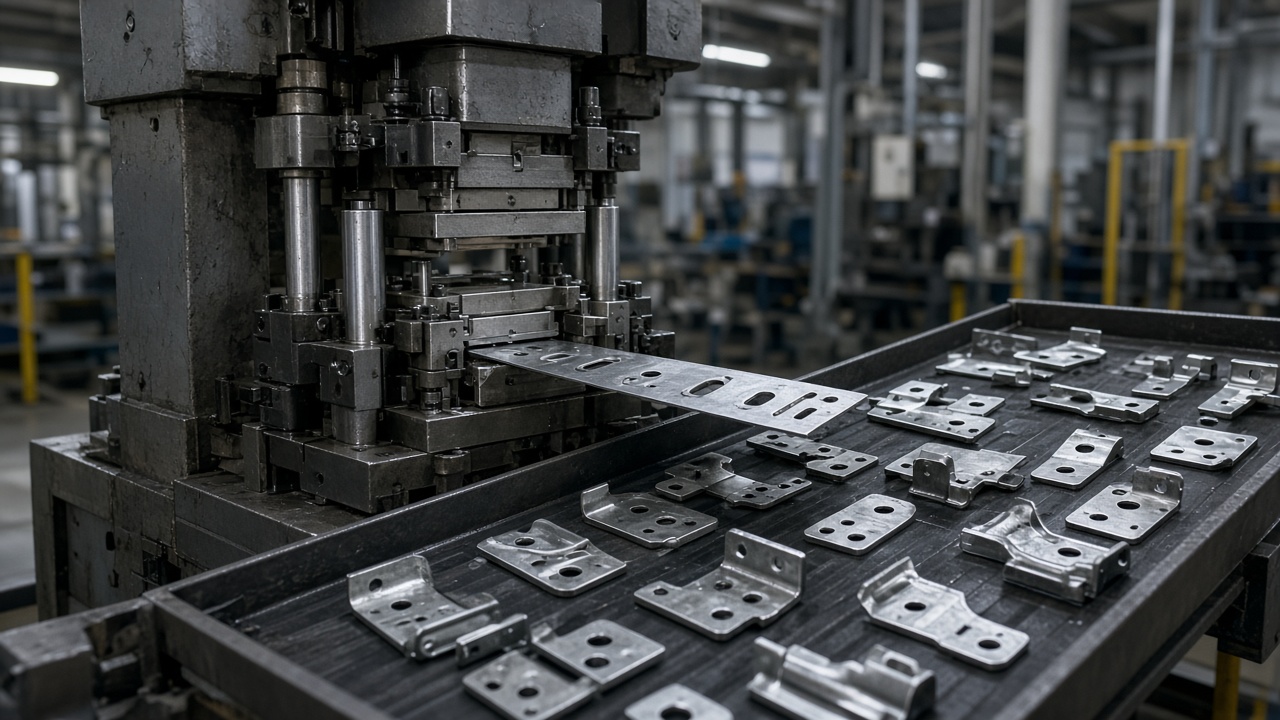
Stamping uses dies to blank and form repeating sheet parts efficiently.
Choose stamping when volume supports tooling versus laser+bend.
Partsproto can bridge with laser while dies are built.
- → Higher annual volumes
- → Repeat brackets/clips
- → In-die forms
- → Cost-down after pilot
DFMのヒント
- •Design for progressive strip when possible.
- •Avoid features that need secondary laser forever.
- •Call burr direction and cosmetic faces.
- •Plan plating before/after pierce carefully.
- •Freeze revisions before hard tooling.
検査と品質
- ✓FA dimensional report.
- ✓In-process checks on critical forms.
- ✓Coil lot traceability when ordered.
- ✓Cosmetic criteria for class A faces.
リードタイムとロットサイズ
Tooling dominates schedule; piece production is fast after approval. Request tool + 1k / 10k / 50k breaks.