Metal 3D Printing (DMLS / SLM)
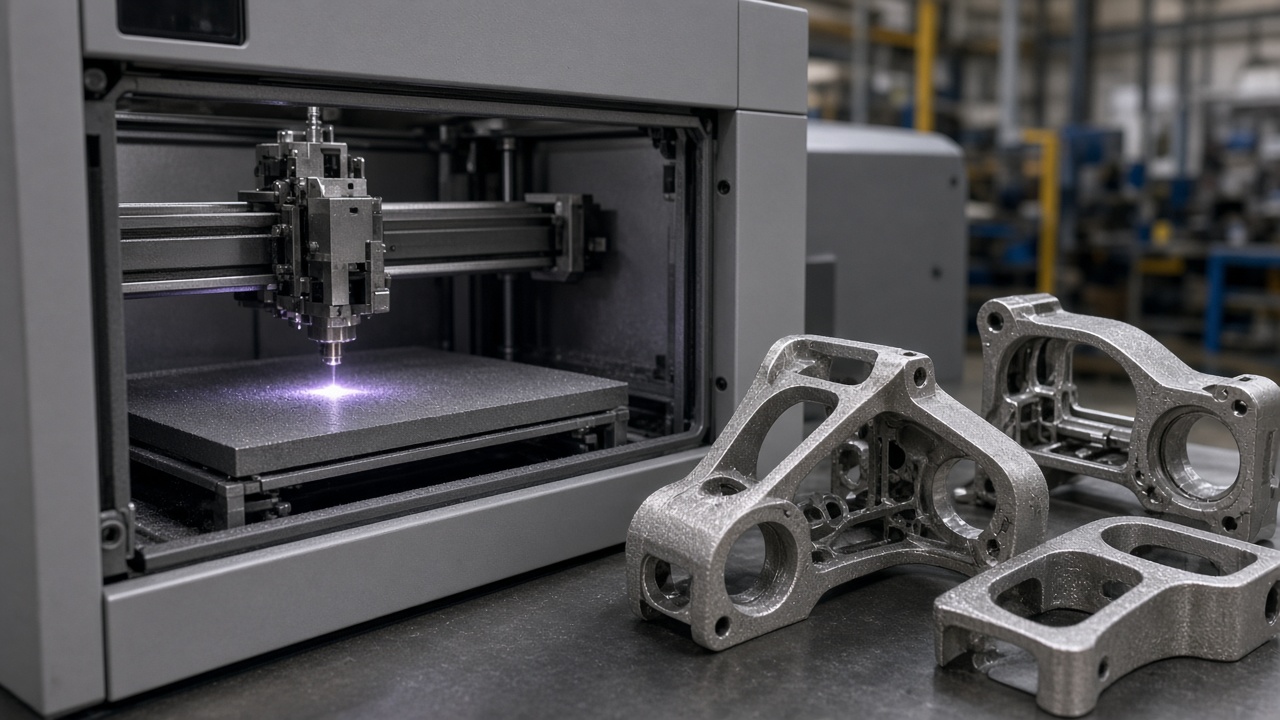
We provide metal powder-bed additive for complex geometries—internal channels, lattices, and consolidated parts—in stainless, aluminum, and titanium alloys. Post-machining and heat treat quoted when needed.
Core Advantages
Practical reasons buyers choose metal AM for prototypes and short-run parts.
Complex Metal Geometry
Hard-to-machine features
Channels, lattices, consolidations
- •Internal cooling paths
- •Topology options
- •Fewer assemblies
- •Custom brackets
Alloy Options
Common engineering metals
SS, Al, Ti and more
- •316L / 17-4
- •AlSi10Mg
- •Ti-6Al-4V
- •Project alloys
Hybrid Manufacturing
Print + CNC
Additive near-net + machining
- •Datum faces
- •Threads
- •Sealing surfaces
- •Tight fits
Lightweighting
Where design allows
Lattices & thin walls
- •Mass reduction studies
- •Stiffness tuning
- •Conformal features
- •Part count reduction
Prototype to Pilot
Without hard tooling
Metal parts before cast/forge
- •Functional metal prototypes
- •Fixture metals
- •Spare complex parts
- •R&D builds
Export Programs
China to overseas
Clear RFQ packaging
- •Alloy + heat treat notes
- •FAI options
- •Packing
- •Freight
What we provide for metal AM
Metal AM Builds
Powder-bed fusion for stainless, aluminum, titanium.
Design review
Support, orientation, and powder escape
Parameter notes
Density and surface expectations
Heat treat
Stress relief / aging when specified
Post-Machining
Critical fits and sealing faces machined after print.
CNC datums
Face and bore CTQs
Threads
Cut or helical options
Surface finish
Machine vs as-built callouts
Inspection
Dimensional and material documentation when ordered.
CMM / gauges
Material certs
Density notes
Photos
Industries & Use Cases
We provide parts for commercial and industrial buyers. Soft capability language—no overclaimed regulated certifications unless stated on the PO.
Industrial Equipment
Complex manifolds and brackets.
- •Manifolds
- •Nozzles
- •Custom mounts
- •Tooling inserts
Energy & Fluid
Flow components—commercial programs.
- •Impeller pilots
- •Housings
- •Channel plates
- •Adapters
Robotics / Automation
Lightweight end-effectors.
- •EOAT
- •Sensor brackets
- •Custom frames
- •Prototypes
R&D / Product Dev
Metal prototypes before casting.
- •Form & fit metal
- •Thermal trials
- •Assembly reduction
- •Pilot builds
Materials
Common grades we process; availability confirmed on quote.
Stainless
- • 316L
- • 17-4 PH
Aluminum
- • AlSi10Mg
- • Other Al (project-based)
Titanium
- • Ti-6Al-4V
Other
- • Tool steels (project)
- • Nickel alloys (project)
- • Copper alloys (project)
Quality & Inspection Notes
Practical QC aligned to RFQ callouts—not blanket aerospace claims.
Build review
Orientation and support strategy checked before run
Post-process control
Heat treat and HIP when ordered
Machining QC
CTQs verified after secondary CNC
Material docs
Alloy certs when required on PO
Soft capability stance
No blanket aerospace/nuclear chamber certifications claimed
Our Process
CAD & alloy select
Share STEP, alloy, heat treat, and CTQs
DFM & quote
Supports, distortion risk, and machining plan
Print & thermal
Build, stress relief / heat treat as ordered
Machine & finish
CNC datums, threads, surface finish
Inspect & ship
FAI notes when ordered; export pack
Frequently Asked Questions
When is metal AM better than CNC?
Internal channels, extreme consolidation, or geometries that need many setups. Simple prismatic parts usually stay CNC.
Do as-built surfaces need machining?
Often yes for sealing faces, bearings, and threads. Call CTQs.
Which alloys do you provide?
Commonly 316L, 17-4, AlSi10Mg, Ti-6Al-4V; others project-based.
Heat treatment?
Stress relief and aging available when specified for the alloy.
Density / porosity?
Process aims for high density; critical pressure parts need explicit requirements and testing on the PO.
Lead time?
Longer than polymer AM—print + thermal + machine. Ask for schedule.
Aerospace certifications?
We do not claim blanket aerospace or nuclear AM certifications. Soft capability language for industrial/commercial buyers.
Cost drivers?
Height, support volume, alloy, heat treat, and machining time.
Metal AM (DMLS/SLM)—service overview
Metal powder-bed fusion builds near-net complex parts in engineering alloys.
Choose metal AM when CNC setups explode or internal features are required.
Partsproto provides print + post-machine workflows from China for overseas buyers.
- → Internal channels
- → Consolidated metal assemblies
- → Lightweight lattices
- → Low-volume complex metal
DFM tips for metal AM
- •Design powder escape holes for hollow sections.
- •Minimize steep overhangs needing heavy supports.
- •Add machining stock on sealing faces.
- •Avoid ultra-thin walls that distort.
- •Call heat treat and hardness targets early.
Inspection & QC
- ✓Dimensional on machined CTQs.
- ✓Visual for build defects.
- ✓Material certs when ordered.
- ✓Optional densitometry / NDT only if PO requires.
- ✓Export packing verification.
Lead time & batch sizing
Plan extra time vs polymer AM. Small brackets may be weeks including machine; complex manifolds longer. Request phased sample then batch.
Ready to Start Your Next Project?
Send CAD, material, finish, and quantity—Partsproto returns process notes, price, and export lead-time guidance.